This guide explains how to evaluate the industrial item code 949841yw334 for consistent procurement quality. It provides objective background on how part identification works, why supplier reliability matters, and what documents you should request. Readers will learn practical conditions and requirements, compare purchasing approaches, and review expert FAQs for lower risk buying decisions.
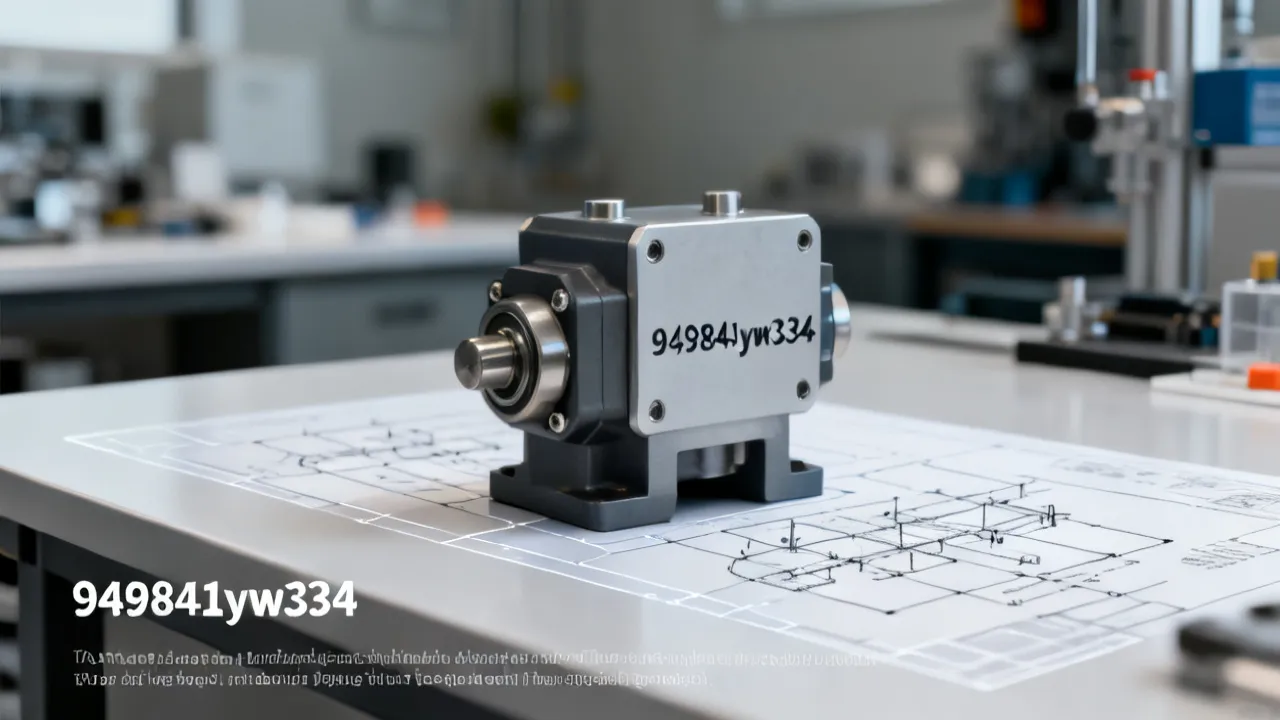
When sourcing the industrial identifier 949841yw334, your goal should be straightforward: confirm the item’s exact specification, validate supplier capability, and align commercial terms with operational needs. This guide is written to help you do that in a disciplined, verifiable way—especially when the additional keywords provided are placeholders that may map to model families, compatibility groupings, or internal catalog references. Focus on traceability, documentation, and test/inspection readiness before you commit to quantity and delivery schedules.
Industrial parts rarely fail because the “name” was wrong; they fail because the underlying specification is subtly different—tolerances, materials, surface treatments, revision level, packaging standards, or compliance requirements. For that reason, 949841yw334 should be treated as a starting point for verification rather than a complete description of the part. If you are also working with related shorthand keywords (as placeholders in your prompt), consider them as likely pointers to compatibility classes—useful, but not sufficient on their own.
In procurement reality, “label match” is often the fastest step and also the most misleading. A label can remain the same while the internal drawing revision changes; it can remain similar across regions while coatings or hardness targets shift; and it can remain identical across packaging lines even when lot traceability processes differ. That is why 949841yw334 must be validated as part of an end-to-end chain: the identifier must map to a specific drawing/spec revision, which must map to a documented manufacturing process, which must map to measurable inspection criteria, which must map to batch-level traceability on the actual shipment.
From an industry perspective, the most reliable procurement process combines:
When done well, this approach makes procurement “audit-ready.” When done poorly, it turns into detective work at receiving—where you discover that the part is functionally close but not assembly-correct, or that documentation exists but does not correspond to the shipment you received.
Think in terms of risk categories. If you address these early, you reduce downstream cost and production interruptions.
To evaluate risk more concretely, you can score each category along two dimensions: likelihood and impact. For example, if 949841yw334 is safety- or reliability-critical, impact is high even if likelihood is low. If it is a low-cost consumable with minimal assembly effect, likelihood may be more important than impact. Either way, your procurement plan should explicitly state how you will reduce each relevant risk.
Another way to view the risk map: there are risks in upstream information (the supplier’s description of the item), manufacturing output (the real properties of the manufactured part), and downstream verification (how you inspect and accept it). Strong procurement controls exist across all three.
As an industry-oriented purchasing specialist would advise, you should request evidence rather than assurances. For 949841yw334, ask for documents that link the code to a specific technical build.
Request the most current specification set tied to 949841yw334. Depending on the part type, this can include engineering drawings, revision history, bills of materials (BOM), material certifications, and performance test criteria.
When you ask for “the specification,” be specific about what you consider complete. A drawing number without a revision is not sufficient. A BOM without material grades is not sufficient. A performance test criterion without the test method reference is often not sufficient. The aim is to obtain a package that allows both technical comparison (to your internal requirements) and verification at receipt (so you know what to measure and how to interpret it).
If your company uses internal engineering controls—such as an ERP/BOM structure, a PLM system, or a document control portal—ask the supplier to reference the same revision baseline or to provide a crosswalk between their drawing revision nomenclature and yours. Even when systems differ, the important thing is traceability to a revision-definitive document set.
Ask what inspection is performed and how it is measured. In practice, suppliers typically can provide:
Evidence can mean more than “we follow a standard.” You want to see the standard applied to your part and your shipment. For example, you may request:
If your industry has formal quality frameworks (e.g., requiring PPAP/PSW documentation, control plans, or specific test assurance strategies), ask the supplier to confirm whether they follow those frameworks and to provide the relevant artifacts. Even when they do not use those exact terms, you can still request the underlying deliverables: control plan, process verification, and evidence tied to the order.
For items identified as 949841yw334, traceability is essential. Ensure the supplier can trace material lots and manufacturing batches to the specific shipment, and that labeling matches your receiving procedures.
Traceability often has multiple layers:
It’s also important to align traceability granularity. For instance, your receiving inspection may accept documentation at carton level, while your internal audit might require lot-level traceability. Before shipment, confirm what granularity you will receive and whether it matches your internal requirement. If not, you may need to alter how the supplier packages or labels the order.
Many procurement failures at the dock are preventable. Confirm packaging standards: protective coverings, moisture control, shock resistance, labeling durability, and the method used to prevent mix-ups between revisions.
Packaging is not just about preventing physical damage; it is also about preventing identity errors. Two practical examples:
Ask about packaging materials and handling instructions. For example, if the part is sensitive to moisture (e.g., corrosion-prone metals or components that require controlled storage), ensure desiccants and proper moisture barriers are used. If the part is fragile or has tight tolerances affecting assembly, request vibration-resistant packing and protective end caps where appropriate.
You mentioned “price information” and “supplier details,” but no explicit numbers or company names were provided in your prompt. In professional procurement, you should still ensure price clarity is concrete: unit price basis, quantity tiers, shipping responsibility, lead time assumptions, and any surcharges. If supplier details are provided in your internal dataset, treat them as candidate sources only until documentation is validated.
Objectively, the procurement decision is typically best supported by side-by-side comparisons of supplier terms and quality evidence rather than by price alone.
To make commercial terms safe and enforceable, incorporate clarity on:
When a procurement contract does not clearly define remedies, you may end up paying for rework even when the supplier was at fault. Therefore, align commercial terms to the acceptance and inspection criteria you plan to enforce.
Your prompt includes additional keywords that appear as placeholders (e.g., 949841yw334 surrounded by blank quoted entries). In real procurement catalogs, those placeholders often represent one of the following:
The best practice is to request an explicit mapping from each keyword you use to the supplier’s technical identifiers and revision levels. Your target outcome is a single authoritative specification for what you are purchasing under the 949841yw334 identifier.
Practically, this means creating a “mapping table” in your procurement request. For each placeholder keyword you provide, ask the supplier to respond with:
Without mapping, you can end up purchasing multiple variants that share an identifier in your system but differ in supplier execution. That makes quality assurance and returns far more complicated than necessary.
Also consider version control on your side. If you have updated internal ERP items, ensure your purchasing team references the correct revision-specific ERP record. Avoid the common trap of using a legacy master record and assuming the supplier will deliver the newest version.
Procurement teams generally consider several approaches. Each can work, but each creates different requirements.
| Approach | Best for | What you should demand | Conditions / requirements |
|---|---|---|---|
| Direct sourcing from manufacturer or authorized channel | When revisions, documentation, and traceability are critical | Revision-specific drawing package, material certifications, inspection reports, batch traceability | Confirm authorization status (if applicable), and ensure revision alignment with your BOM |
| Specialist distributor sourcing under your part code | When lead time and access to multiple supply options matter | Stock/availability evidence, certification documents for the specific shipment, return policy terms | Require documentation prior to shipping and validate packaging/labeling practices |
| Alternate supplier qualification | When you need cost optimization or supply resilience | Capability evidence, agreed inspection plan, PPAP-like documentation where relevant | Run a controlled first-article or trial batch, then lock acceptance criteria in writing |
To make the comparison actionable, define what “best for” means in your context. For instance, if you must produce quickly, distributor stock might look attractive—but you must still ensure documentation corresponds to the specific stock lot. If documentation is generic or dated, the distributor might still be a risk.
Similarly, alternate supplier qualification can be cost-effective but can introduce transitional risks: process control differences, measurement calibration differences, and documentation mismatches. The solution is not to avoid alternate sourcing, but to impose a qualification plan that forces evidence rather than promises.
It can also be useful to create an internal “supplier evidence baseline.” For example, for 949841yw334 your baseline might always include: revision-specific drawing, material certificate, dimensional inspection report, and traceability fields matching your receiving database. When you evaluate an approach, ask whether it can reliably meet that baseline every time.
The following workflow is designed to minimize ambiguity and provide the structure procurement teams commonly need for audit-ready decisions.
To strengthen this workflow, add a short internal step: create a “receiving package” before shipment arrives. That receiving package typically includes your checklist, drawing references, measurement tools/calibration status, acceptance thresholds, and an escalation path for nonconformance. If receiving happens in a hurry, the receiving package is what prevents errors.
Also, consider establishing communication discipline. Procurement teams often exchange emails or tickets; receiving teams may not see those threads. You can avoid this by requiring that the supplier’s documentation and revision confirmation are attached to the purchase order record, not just sent via a separate message.
Even with the correct code 949841yw334, procurement outcomes depend on conditions that buyers sometimes overlook.
One common “hidden condition” is tooling or process variation. Even if the drawing revision is the same, the supplier might alter process parameters, subcontract steps, or inspection locations. If you suspect this risk, require the supplier to disclose their process control approach and to notify you of any process changes that could impact form/fit/function.
Another hidden condition is measurement capability. If your inspection plan requires critical dimensions, ensure the supplier’s capability supports those dimensions. In practice, you can ask about their capability indices (e.g., Cp/Cpk) when appropriate, or you can mitigate by requiring additional incoming inspection for the trial order.
Finally, procurement success depends on whether your internal team uses consistent revision control. If your internal BOM references the correct revision but your receiving record references a generic part, you may accept the wrong variant inadvertently. Align ERP/BOM, receiving, and quality systems to the same revision-specific identifiers.
No. 949841yw334 should be treated as an identifier that must be mapped to a specific technical specification and revision level. You still need documentation such as drawings, material certificates, and the supplier’s inspection evidence.
Request revision-specific engineering documentation, material certifications (where relevant), inspection/test reports for the specific shipment, and traceability details that link the production batch to your order. If applicable to your industry, ask for compliance statements tied to the part’s use case.
For many procurement teams, a “first order” request should also include a control plan or equivalent description of how the supplier manages the critical-to-quality characteristics. Even a concise list of what they measure, how they measure, and acceptable tolerances can dramatically reduce uncertainty.
Require the supplier to reference revision identifiers from their drawing system and provide a spec match confirmation. Where possible, request first-article verification results or trial-batch inspection before switching to full-volume purchasing.
To make this more reliable, require both suppliers to provide the same set of evidence: the drawing reference, the revision level, the material certificate reference, and a shipment-specific inspection report. Then compare them side-by-side. If one supplier provides more or better evidence, do not assume the other supplier is wrong—assume they may be incomplete and ask for missing artifacts.
Require a documented equivalency assessment: material differences, dimensional impacts, performance changes, and test implications. Then update your acceptance criteria accordingly. Do not rely on verbal “fit” statements.
In a substitution scenario, you should also clarify what happens if the substitute meets your acceptance criteria in isolation but fails in system-level assembly (for example, because of tolerance stack-up). Your equivalency assessment should therefore consider interface geometry and system integration needs, not only component-level pass/fail results.
Use a receiving checklist tied to your acceptance plan: verify labeling, part marking, revision identifiers, packaging integrity, and perform dimensional or functional checks upon receipt. Include these requirements in your purchase order.
It also helps to verify the supplier’s packing list. Compare the packing list contents and identifiers against the physical markings on the containers. If there is any mismatch, stop receiving and initiate a discrepancy review. The cost of investigation early is typically far lower than the cost of discovering the mismatch after parts have entered production.
Price alone is rarely sufficient. Consider total delivered cost and procurement risk: documentation quality, inspection reliability, lead time consistency, return policies, and the supplier’s capacity for revision control. A slightly higher price can be economically rational if it reduces rework and downtime.
To operationalize this, implement a “total cost of quality” approach. Total cost includes not only unit price and shipping, but also the cost of inspection labor, rework scrap, and schedule risk. Even a small reduction in risk can outweigh a small unit cost difference.
At minimum, include the exact identifier 949841yw334, revision-specific references, required documents/certificates, delivery terms, packaging requirements, inspection/acceptance criteria, and clear replacement/returns conditions in case of nonconformance.
It can be useful to attach a “quality clause” to the PO. This clause references the required documents, acceptance plan, and the supplier’s responsibility for providing shipment-specific evidence. Without such a clause, enforcement becomes difficult when disputes arise.
Not necessarily, but it depends on supplier history and how stable the manufacturing process and revision control are. After qualification and when revision control is stable, you can transition to periodic sampling aligned with your risk assessment.
A practical approach is to define qualification frequency rules. For example, you might require FAI again when a supplier changes a critical process step, when a new revision is introduced, or after a long factory downtime event. Otherwise, you can move to routine sampling and rely on ongoing documentation plus receiving checks.
From a governance standpoint, procurement teams increasingly treat supplier selection and qualification as a managed process rather than a one-time event. In many manufacturing environments, internal audits expect evidence that the supply chain can maintain consistent quality over time. That expectation is exactly why 949841yw334 should be anchored to verifiable documentation and acceptance criteria, not only to an identifier.
If your organization operates under formal quality management practices, your supplier evaluation should consider: traceability completeness, audit readiness, corrective action performance, and the clarity of technical documentation. Even without referencing any industry-specific numbers, the procurement logic remains stable: quality assurance is a system, not a promise.
Supplier governance also matters because of how changes propagate. A supplier might change subcontractors, switch material sources, update manufacturing equipment, or alter their inspection tooling—all while keeping the same outward part name. Governance processes require those changes to be communicated and assessed before they affect your output.
For 949841yw334, a governance-friendly approach includes:
If you want to make the checklist more operational, convert it into a receiving form with checkboxes and signature fields. For example, include boxes for “label revision matches,” “packing list matches,” “dimensions verified,” “functional check passed,” and “documents reviewed and filed.” This reduces ad-hoc decisions and makes compliance easier during internal audits.
Another practical improvement is to ensure your team has the right measurement tools and calibration status. If the acceptance plan requires a measurement you can’t reliably perform, you might accept incorrectly or unnecessarily reject conforming items. Align procurement and quality planning so that inspection readiness exists before delivery.
Your prompt references price and supplier details, but no explicit values were supplied. If you are currently missing those inputs, the most objective next step is to structure your inquiry so that suppliers respond with consistent data. When you request quotes for 949841yw334, ask for:
This approach makes supplier comparisons fair and reduces the likelihood that negotiations become dependent on incomplete information.
To reduce back-and-forth, attach a “quote request package” with your requirements. That package can include the identifier 949841yw334, the required revision (if known), your acceptance criteria references, and a list of required documents. Suppliers that respond completely and consistently are usually easier to work with long-term, because their documentation practices are already aligned with your procurement needs.
Also, be careful about lead time communication. Some suppliers quote lead time for production only, while you may still need time for documentation approval and receiving inspection. Decide whether lead time includes documentation delivery. If it does not, require documentation to be shipped along with the parts or delivered by an agreed date ahead of the shipment.
Buying industrial components under the identifier 949841yw334 is best approached as a specification-and-evidence task. By validating revision alignment, requiring traceable documentation, and agreeing on acceptance criteria before shipment, procurement teams can reduce technical fit failures, quality surprises, and receiving delays. The result is a sourcing decision that stands up to operational scrutiny—whether you are purchasing through a direct channel, a distributor, or a newly qualified supplier.
When you treat 949841yw334 as a traceable identifier tied to revision-specific evidence—not as a casual “catalog name”—you make procurement safer. You also protect production schedules and reduce the administrative cost of disputes, rework, and returns.
Request compatibility confirmation based on interface geometry and tolerances relevant to your assembly. If your additional placeholders correspond to interface categories, ask the supplier to map each category to the technical spec they are using for 949841yw334.
Compatibility is often a tolerance problem disguised as a “fit” problem. To handle it safely, you can require:
If you do not have the full mating component drawings (e.g., because they are supplied by other vendors), ask your supplier what they consider critical interface dimensions and how those dimensions are controlled. Then, within your internal process, validate your assembly clearance and functional criteria using the parts you receive.
Common red flags include: refusal to provide revision-specific documentation, vague inspection claims without reports, inconsistent labeling/traceability practices, unclear returns policies, or substitution offers without documented equivalency impacts.
Other red flags include:
If you see these red flags, do not necessarily reject the supplier immediately. Instead, escalate your requirements: demand evidence tied to the shipment and require a controlled trial order. Many suppliers can correct these gaps when they understand that your acceptance process is evidence-driven.
For first-time sourcing, start with a controlled trial or qualification batch aligned with your acceptance criteria. Then scale the order only after successful receiving checks and documentation review for 949841yw334.
Cost-effective doesn’t always mean cheapest unit price. A trial batch can prevent expensive downstream costs: assembly line stoppage, scrapped inventory, and engineering time spent on root cause analysis.
To keep the trial cost under control, you can define a “minimum documentation and testing scope” for the trial order. For example:
Once the trial order demonstrates compliance, you can reduce incoming inspection burden through risk-based sampling while continuing to require shipment-specific CoCs and traceability information.
Yes. You can define inspection dimensions, tolerances, sampling approaches, and functional testing requirements in your purchase documentation, provided the supplier can execute them. This reduces ambiguity at receipt and creates measurable acceptance boundaries.
To implement inspection standards safely:
When acceptance criteria are clear and enforceable, supplier disputes become less subjective. Instead, outcomes become measurable and based on documented evidence.
If the supplier provides documentation but it does not match the shipment identifiers or revision references, treat it as a nonconformance until resolved. Do not accept the shipment based solely on physical appearance. The safe action is to quarantine the parts (per your internal procedure), verify label/markings against the packing list, and require the supplier to provide corrected, shipment-specific documentation.
Common causes include file mix-ups, data entry errors, and certificates generated from prior shipments. Ask the supplier for a revised documentation set tied to the shipment’s lot/batch numbers. If documentation mismatch repeats, reevaluate supplier governance and consider more stringent evidence requirements for future orders.
When nonconforming items are found, your process should already be defined in the purchase order and acceptance plan. Typically, you should:
In safe procurement, disputes are reduced by having a pre-agreed remedy. Without it, resolution can become slow and costly.
Revision surprises happen when suppliers update parts without proper notification or when your internal systems are not aligned with the latest approved revision. To prevent this:
This transforms revision control from a hope into an enforced step.
Yes. Risk-based inspection allows you to reduce cost while maintaining safety. After qualification, you can move from full inspection to sampling—provided that you have:
If the supplier performance changes or documentation becomes inconsistent, you can increase sampling again or reintroduce verification for critical dimensions. The key is to tie inspection level to measurable performance, not to convenience.
For audit readiness and continuous improvement, maintain records across the procurement lifecycle:
This record set helps you respond quickly when questions arise—whether internal audits, customer audits, or quality investigations.
Create an evidence bundle that includes both “what you asked for” and “what you received.” A typical audit-friendly bundle might include:
When this bundle is complete, it becomes easy to demonstrate that procurement decisions were made safely and that acceptance was performed against documented criteria.
Communication clarity is a procurement control. Use structured requests rather than informal notes. For example, send a quote request that includes:
When suppliers receive this structure, it reduces the chance of incomplete quotes or generic documentation that later fails to satisfy your acceptance process.
In general, no. Placeholders may represent compatibility classes, family markers, internal routing codes, or spec category tags. Even if 949841yw334 is correct, placeholders can indicate differences in allowable variants or interfaces.
The safe approach is to map every placeholder to the supplier’s technical identifiers and to confirm that the supplier’s manufacturing and inspection align to the specific variant you need. Ignoring placeholders is a common cause of subtle misprocurements.



This guide explains how Vidapono and xivdapono are commonly discussed as holistic wellness concepts, focusing on responsible sourcing and product-evaluation habits. It provides objective background on the terms, typical categories of related products, and practical ways to compare claims, supplier credibility, and quality indicators. Readers will learn what to verify before purchase.
This guide explains how to evaluate the industrial item code 949841yw334 for consistent procurement quality. It provides objective background on how part identification works, why supplier reliability matters, and what documents you should request. Readers will learn practical conditions and requirements, compare purchasing approaches, and review expert FAQs for lower risk buying decisions.
This guide explains how to assess supplier options, compare pricing, and verify product or service fit before committing. It provides objective background on the concepts behind supplier selection—such as lead time, quality controls, documentation, and cost drivers—using clear decision criteria. The goal is practical, repeatable evaluation rather than guesswork or marketing claims.
Esta guía analiza, con enfoque experto y objetivo, cómo abordar decisiones de atención centradas en Mulleres y su entorno de necesidades. Se revisan fundamentos del concepto, factores de calidad, criterios de evaluación y requisitos habituales. El texto ofrece una guía práctica y una comparación para orientar elecciones informadas, sin suposiciones ni promesas difíciles de verificar.
This guide explains how to evaluate “Sdfbn” and related supply options with an objective, step-by-step approach. Background: the keywords “Sdfbn” and surrounding terms are treated here as placeholders for a product/service category, so readers learn practical evaluation criteria without relying on marketing claims. The focus remains on supplier credibility, pricing structure, and compliance readiness.
This guide explains how Tumnbj mmlcjowm is discussed in industry channels and how “nearby” buyers typically evaluate it against practical constraints. It also presents background context for the terms, common sourcing behaviors, and decision factors that shape supplier selection, timeline expectations, and verification requirements—using an objective, process-oriented approach suitable for procurement and operations readers.

